How to Choose an Ultrafine Ball Mill?
Choosing an Ultrafine Ball Mill is not a matter of selecting the smallest machine. It is a process decision involving feed size, mineral hardness, moisture, target fineness, capacity, and energy use. A mill that produces beautiful laboratory powder may struggle beside a continuous production line. That difference matters.
Fred C. Bond remains an important authority in grinding engineering. His well-known statement says, “The work input required to reduce the size of a given quantity of material is inversely proportional to the square root of the product size.” This principle helps engineers estimate energy demand, but it should not replace pilot testing. Real materials contain impurities, moisture, and uneven particles. These details can change performance quickly.
A reliable selection process begins with measurable evidence. Record the feed size distribution. Test the material’s hardness and abrasiveness. Define the required product size, such as D90 below 10 microns. Then compare residence time, media size, liner wear, cooling requirements, and operating cost. Watch the discharge temperature. It can reveal hidden energy losses.
Capacity matters too. A compact Ultrafine Ball Mill may fit neatly into a workshop, yet its throughput could disappoint. A larger model may offer stability but demand more space and maintenance. No choice is flawless. Even experienced engineers can overvalue one specification.
The strongest decision combines supplier data, independent testing, and operating experience. Ask for comparable applications, not impressive photographs. Inspect the powder under a particle-size analyzer. Check whether the results remain consistent after several hours. Small tests often expose large assumptions. This guide explains how to compare these factors clearly and choose equipment with greater confidence.
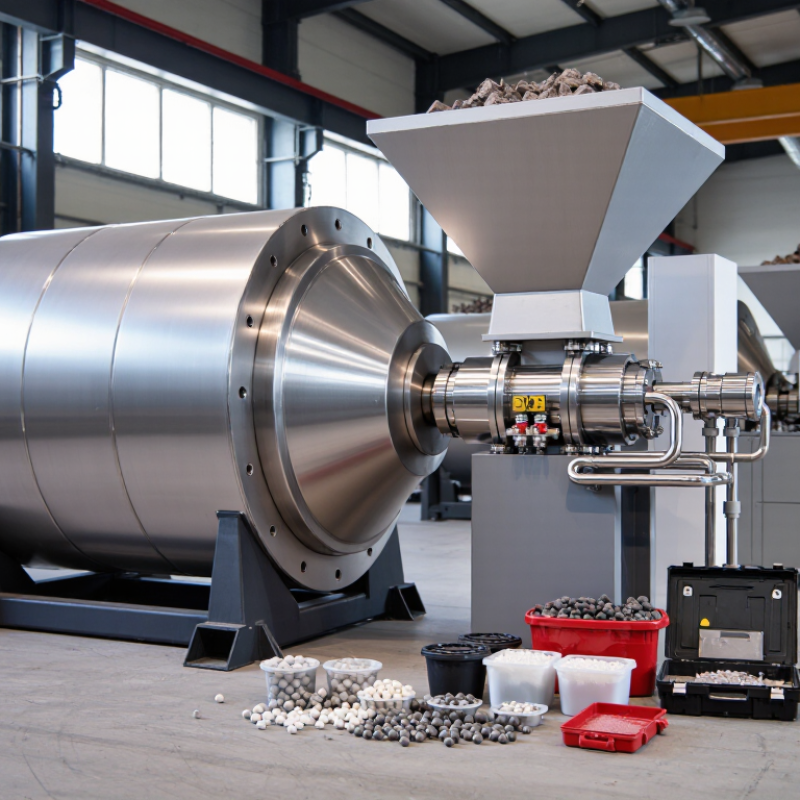
Define the Target: Ultrafine Particle Sizes from D97 5–45 μm
Choosing an ultrafine ball mill begins with a measurable particle-size target. If your specification is D97 5–45 μm, define the exact value before comparing equipment. D97 means 97% of particles are smaller than the stated diameter. That figure is not the same as average size. A powder with a 20 μm median can still exceed a 45 μm limit. Measure the feed with a validated laser-diffraction method. Record moisture, hardness, and feed size. Small details matter.
A 5 μm target demands tighter classification and more controlled grinding than a 45 μm target. The mill must provide stable energy input without excessive heat or contamination. Ask for test data using your actual material, not a generic mineral sample. Check the achieved D97, production rate, specific energy, and temperature rise. Inspect samples from several time points. One clean sample proves little. Classifier settings, media loading, and residence time can shift the result.
For sticky or moisture-sensitive feed, drying may be necessary before fine grinding. Hard feed may require staged size reduction to protect output and operating stability. Test the powder. Compare particle curves, not only one D97 number. I would not promise 5 μm production from a small laboratory test without scale-up evidence. Real plants introduce wear, airflow changes, and feed fluctuations. Those problems are easy to underestimate. Build a trial plan with acceptance limits, sampling intervals, and procedures for handling out-of-specification batches.
How to Choose an Ultrafine Ball Mill? — Define the Target: Ultrafine Particle Sizes from D97 5–45 μm
D97 indicates that 97% of the processed material is finer than the stated particle size. Select the mill and classifier configuration according to the required target rather than choosing equipment by nameplate capacity alone.
The chart shows practical target setpoints within the D97 5–45 μm ultrafine range. Lower targets generally require higher specific energy, more effective classification, and closer control of feed moisture, hardness, and mill loading. Actual results depend on the material and process conditions.
Match Mill Types to Hardness, Feed Size, and Mohs Ratings up to 9
How to Choose an Ultrafine Ball Mill?
Choosing an ultrafine ball mill starts with the material, not the machine label. Hardness matters. A soft mineral may reach fine sizes with moderate energy and standard grinding media. Materials near Mohs 9 demand tougher media, durable liners, and careful control of contamination. Ceramic or hardened grinding components can reduce metal pickup, but they may increase operating costs.
Feed size also controls mill performance. A mill designed for ultrafine grinding should not receive oversized lumps without preparation. In practical testing, I check the feed distribution, moisture, and the required final size before selecting equipment. A feed below a few millimeters often gives more stable results than irregular coarse particles. Wet grinding can help control dust and temperature, while dry grinding may simplify downstream handling. The choice depends on the process.
For laboratory work, a planetary or vibratory design can provide strong impact energy for small batches. Continuous stirred media systems may suit larger output and narrow particle distributions. When processing hard materials up to Mohs 9, I monitor media wear, motor load, temperature, and particle size during each trial. Do not trust hardness data alone. Impurities, cracks, and moisture can change grinding behavior. One test may look excellent, yet fail during extended operation. I would compare at least two media sizes and inspect the final powder for contamination before approving the mill.
Select Ball Diameter, Liner Materials, and Media Filling Ratios
How to Choose an Ultrafine Ball Mill?
Selecting ball diameter is the first practical decision. Large balls deliver stronger impact and suit coarse, hard feed. Small balls create more contact points for ultrafine grinding. A mixed charge often performs better than one size. For example, larger media can break 5-millimeter particles, while smaller media refine the remaining powder. Test the feed before fixing the final ratio.
Liner materials affect wear, contamination, and operating stability. A high-hardness liner may resist abrasive minerals, but it can introduce unwanted elements if chipping occurs. Ceramic liners reduce metallic contamination, although they may crack under severe impact. Check slurry chemistry, temperature, and cleaning requirements. Inspect the liner after each trial. Small grooves can change the grinding pattern.
Media filling ratio needs careful adjustment. Many applications begin near 30 to 40 percent of the chamber’s working volume. Too little media reduces collision frequency. Too much media can restrict movement and increase motor load. Measure the actual charge, not the pile’s appearance. Monitor product fineness, power draw, temperature, and noise together. A quiet mill is not always an efficient mill. In my view, the best setting is rarely the first setting tested. Particle-size results may improve while energy use becomes unacceptable. Record both outcomes, then adjust ball diameter, liner choice, and filling ratio as one system.
Compare Capacity, Energy Use of 20–100 kWh/t, and Classifier Efficiency
How to Choose an Ultrafine Ball Mill?
Capacity and energy use should be judged together, not separately. A mill producing ten tonnes per hour may consume more power per tonne than a slower unit. Target fineness, feed moisture, and hardness strongly change the result. Compare test data at the same product size. Numbers need context.
Energy demand can range from 20 to 100 kWh/t in ultrafine grinding. Lower consumption is attractive, but it may indicate coarser product or incomplete liberation. Ask for net energy figures, including the classifier and air system. Measure power over a stable operating period. Short trials can hide fluctuations. I have seen initial estimates fail when wet feed entered the circuit. Test the feed.
Classifier efficiency often determines real capacity. A sharp cut point returns fewer correctly sized particles for further grinding. This reduces overgrinding and can lower circulating load. Watch the fine-particle yield, pressure drop, and reject rate. A classifier operating at 85% efficiency may waste more energy than expected. However, efficiency figures need a defined test method. Some suppliers report ideal laboratory results instead of continuous plant performance. Request particle-size curves, not only one headline value. Leave room for maintenance, liner wear, and seasonal feed changes. The best selection balances tonnes per hour, 20–100 kWh/t energy demand, and stable classification under actual conditions.
How to Choose an Ultrafine Ball Mill? - Compare Capacity, Energy Use of 20–100 kWh/t, and Classifier Efficiency
Representative planning ranges for a dry, closed-circuit mineral-grinding system using a ball mill and dynamic classifier. Actual results depend on feed hardness, moisture, feed size, media filling, mill speed, and product specification.
Target Product
P80 |
Typical Feed
F80 |
Indicative Capacity
(t/h) |
Specific Energy
(kWh/t) |
Classifier Efficiency
(%) |
Typical Circulating
Load (%) |
Recommended Operating Focus |
| 5 μm |
≤1.0 mm |
0.3–1.0 |
80–100 |
85–92 |
200–300 |
Use a high-efficiency classifier, narrow particle-size control, and intensive cooling. Expect the highest energy demand and lowest throughput. |
| 10 μm |
≤1.5 mm |
0.5–1.8 |
55–80 |
88–94 |
180–280 |
A balanced choice for genuine ultrafine production. Prioritize classifier stability and mill ventilation to prevent overgrinding and heat buildup. |
| 15 μm |
≤2.0 mm |
1.0–3.0 |
40–65 |
90–95 |
150–250 |
Often provides the best compromise between capacity, energy use, and product fineness for closed-circuit operation. |
| 25 μm |
≤2.0 mm |
2.0–5.0 |
28–50 |
90–96 |
120–220 |
A practical range when moderate ultrafineness and higher throughput are more important than maximum surface area. |
| 45 μm |
≤3.0 mm |
3.0–8.0 |
20–35 |
92–97 |
100–180 |
Choose this operating range when energy efficiency and capacity are prioritized over a very fine product. |
|
Selection rule: For a target below 10 μm, give priority to classifier efficiency, cooling capacity, and wear control. For targets of 15–25 μm, compare total specific energy and stable throughput. For targets around 45 μm, capacity and energy consumption usually become the dominant selection criteria.
|
Data basis: The ranges are representative engineering benchmarks for dry mineral grinding in a closed circuit, assuming relatively dry feed, controlled mill loading, and a properly adjusted dynamic classifier. They should be validated through laboratory or pilot testing before equipment sizing.
Verify Product Quality, Wear Rates, Safety, and Total Operating Cost
How to Choose an Ultrafine Ball Mill?
Verify product quality before discussing price. Request a factory test report showing feed size, product size, capacity, moisture, and power consumption. A reliable supplier should provide laboratory results, calibration records, and a repeatable sampling method. Compare particle-size data from laser diffraction, not only a single “ultrafine” claim. In practice, a 5% change in moisture can alter mill performance and classifier stability. That detail is easy to overlook.
Wear rates deserve a controlled trial. Measure liner thickness, grinding-media loss, and product contamination after a fixed operating period. CEEC-hosted comminution literature reports that grinding can consume 3–4% of global electricity and represent up to half of a mine’s energy use. Small efficiency losses become expensive quickly. Ask for kWh per tonne at your actual feed condition. Published figures may look excellent, but laboratory conditions rarely match a dusty, variable plant.
Safety and total operating cost must be checked together. Confirm guarding, emergency stops, interlocks, dust extraction, noise controls, and risk assessment procedures aligned with ISO 12100 principles. Inspect maintenance access closely. Measure the hidden losses. Energy, liners, media, labor, filter replacements, and unplanned downtime should enter a five-year cost model. The U.S. Department of Energy’s motor-system guidance also emphasizes that efficient motors alone cannot fix poorly controlled mechanical loads. I would leave a contingency allowance; wear predictions are useful, but never perfectly certain.